Current location: home page > Products > Buried composite pipe for gas stations
Brief description:When there is a large temperature difference between the pipe storage area and the construction site, the pipe fittings should be left on site for half an hour before electric fusion welding. This article explains the impact of temperature difference on welding and the key points of operation.
 News
Why should composite pipes be left for half an hour before electric fusion welding? Direct answer: When transporting pipes between storage and construction sites, if there is a large temperature difference between the two, the surface of the pipe will condense or overheat, carrying condensed water or temperature stress, and directly welded. Water vapor will vaporize at high temperatures, forming pores and greatly reducing the strength of the weld. The standard practice is to place the pipes and fittings at the construction site for at least half an hour before and after connection, allowing the temperature to approach the ambient temperature and the surface to be dry before welding. This step is most easily saved by rushing the schedule during winter and seasonal changes, and it is precisely at this time that it is the most crucial.
Two consequences. One is condensation water: When the cold pipe enters the warm construction site, water droplets immediately condense on the surface, and the welding surface contains water. During electric melting, the water evaporates and produces pores and virtual welding, which cannot be seen from the appearance. It only leaks after pressure testing or operation. The second is thermal stress: when there is a large difference between the temperature of the pipe and the environment, the cooling shrinkage is uneven, and the weld joint bears additional stress during the cooling process, which becomes a crack source after long-term operation. Half an hour of placement is to align the condition of the pipe with the working conditions, with extremely low cost and saving all hidden dangers.
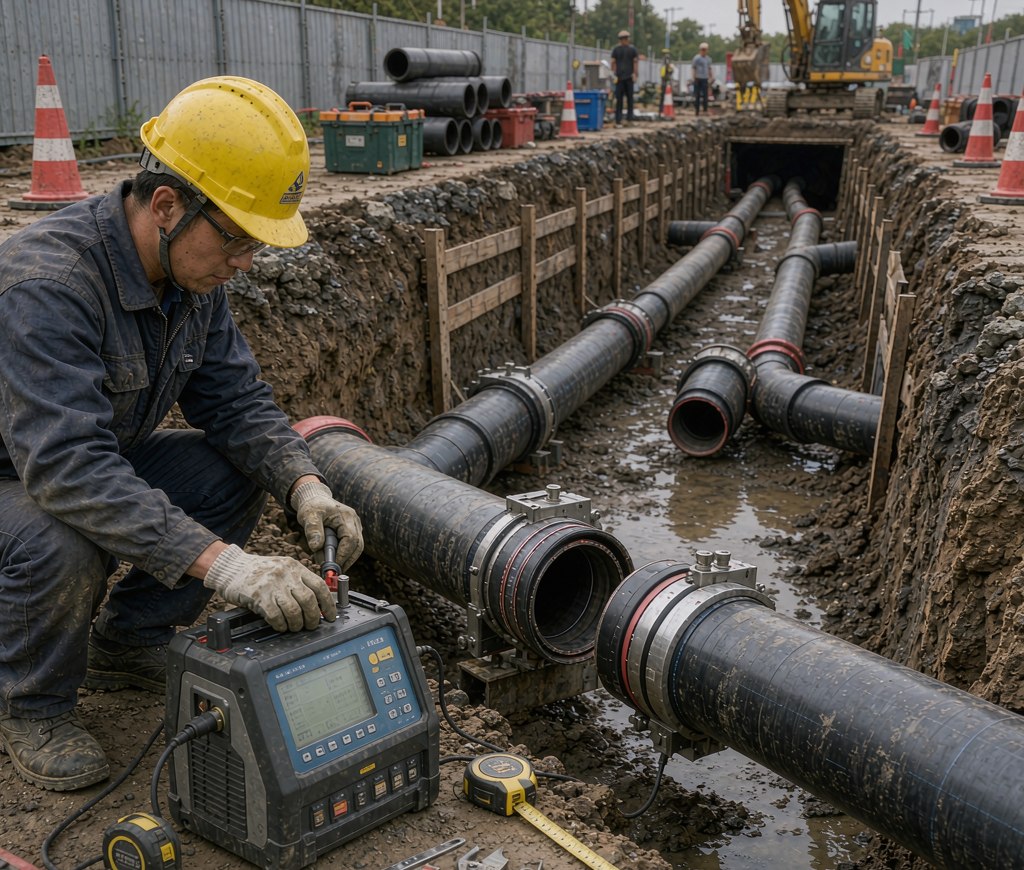
Leaving it for half an hour is just one part of the process. There are still a few steps to complete the preparation: scraping - using a special scraper or a specified mesh of corundum sandpaper to remove the oxide layer in the welding area. The scraping range should be about one centimeter wider than the insertion depth, and the thickness should be based on visible changes; Cleaning - Use a designated cleaning agent soaked in a lint free clean cloth to wipe the outer surface of the pipe insertion end and the inner surface of the pipe fitting, removing oil and dirt; Marking - Use a marker pen to mark the insertion depth, ensuring that the end face is vertical and free of burrs. Prepare a solid weld joint, cool it down, and then tap to check for a dense sound.
The electric fusion welding machine must use specialized equipment provided by the supplier, with parameters set according to the factory settings of the pipe fittings, and should not be adjusted by oneself. During welding, the pipes and fittings should be securely fixed to prevent displacement or protrusion during insertion. It is strictly prohibited to move or test the pressure in advance after welding - the cooling time should be executed according to the regulations, and the uncooled joint will leave residual stress under stress. Record welding parameters and operators for each weld junction, forming a traceable quality file. When installing underground, it is important to remember the principle of minimizing joints: those that can be fully extended do not need short joints, and those that can be welded less should be welded. Each joint is a potential risk point.
| mistake | consequence | The correct approach |
|---|---|---|
| Direct welding due to large temperature difference | Pore virtual welding | On site placement for half an hour |
| Replace the prescribed abrasive with sandpaper | Particle contamination of welds | Use corundum sand cloth with specified mesh size |
| Insufficient scraping range | Residual oxide layer | Extend the insertion depth by one centimeter |
| Move without cooling down | Joint deformation and cracking | Cooling according to regulations |
The quality of the weld seam is not visible - welds with intact appearance may have internal pores. Making every step solid is the fundamental way to ensure that every weld can withstand pressure testing and time testing.
There is still a temperature difference and humidity difference between the warehouse and the outdoor work area. Placing it for half an hour as a standard action is cost-effective and high in safety.
The scraping area reveals a fresh and uniform natural color of the material, and the thickness changes can be visually judged. The range covers the insertion depth and is extended by one centimeter.
It is not recommended to perform pressure repair welding on electric fusion joints. Cut and re weld the joints and analyze the reasons. The reliability of the repaired joints cannot be guaranteed.
This article is organized by Luoyang wohong petrochemical equipment co., ltd. the company provides design, manufacture, installation, commissioning and operation and maintenance services for oil and gas recovery equipment, solvent recovery devices and buried composite pipe networks at gas stations, oil depots and chemical enterprises. if you need scheme configuration or on-site investigation, please contact and exchange.
 Previous articleWhy choose composite pipes for gas station pipeline renovation?
 Company Name:
Luoyang Wohong Petrochemical Equipment Co., Ltd
 Hotline:
13526990215
 Company Address:
W2-1, Dongda Technology Industrial Park, Luoxin Industrial Cluster, Xin'an County, Luoyang City
 E-mail
lixiang@vohonoilpipe.com
Scan to follow us
Luoyang Wohong Petrochemical Equipment Co., Ltd Powered by EyouCms Henan ICP Registration No. 17014668-11 sitemap.xml
 Product Category