Current location: home page > Products > Buried composite pipe for gas stations
Brief description:The composite pipe joint is made using two methods: electric melting and flange. The sealing is done by using oil resistant gaskets and standardized fastening, and the sealing is confirmed by pressure holding tests. This article explains the key process points and acceptance caliber.
 News
How to make the joint of composite pipe? What are the requirements for connecting processes and sealing closed loops? Direct answer: The connection of buried composite pipes in gas stations is mainly done by electric fusion socket, with flange connections for large diameters or parts that need to be disassembled; The core of sealing lies in the proper insertion depth, welding parameters executed according to the pipe process, and no damage to the sealing surface. For flange connections, the oil resistant gasket should be evenly fastened diagonally; After the joint is completed, a closed circuit test must be conducted to ensure that the voltage is stabilized and qualified. The joint is the thinnest part of the sealing chain in the composite pipeline network, and the pipe body does not corrode, with 90% of the leakage occurring at the joint. This article explains the methods, sealing requirements, and testing diameters for two types of connections.
The method of electric fusion socket: the cut of the pipe end is flat and the burrs are removed. The socket depth is marked with a line according to the specifications of the pipe. The oxide layer on the outer surface of the pipe fitting and the pipe end is scraped off to the specified range; The parameters of the electric fusion welding machine are set according to the pipe barcode or process document, and the voltage and cooling time cannot be changed based on experience; During the welding process, keep the pipe fittings stable and strictly prohibit movement and stress during the cooling period. Three common mistakes: inadequate scraping leading to virtual connection of the fusion surface, insufficient insertion depth causing the stress area to be folded, and backfilling or pressure testing before full cooling. After the welding is completed, a resistance or appearance inspection shall be carried out according to the pipe process. The qualified joint shall have a uniform and full outer flange. The welding parameters printed by the welding machine shall be archived with the completion data, and future traceability shall rely entirely on this line of text.
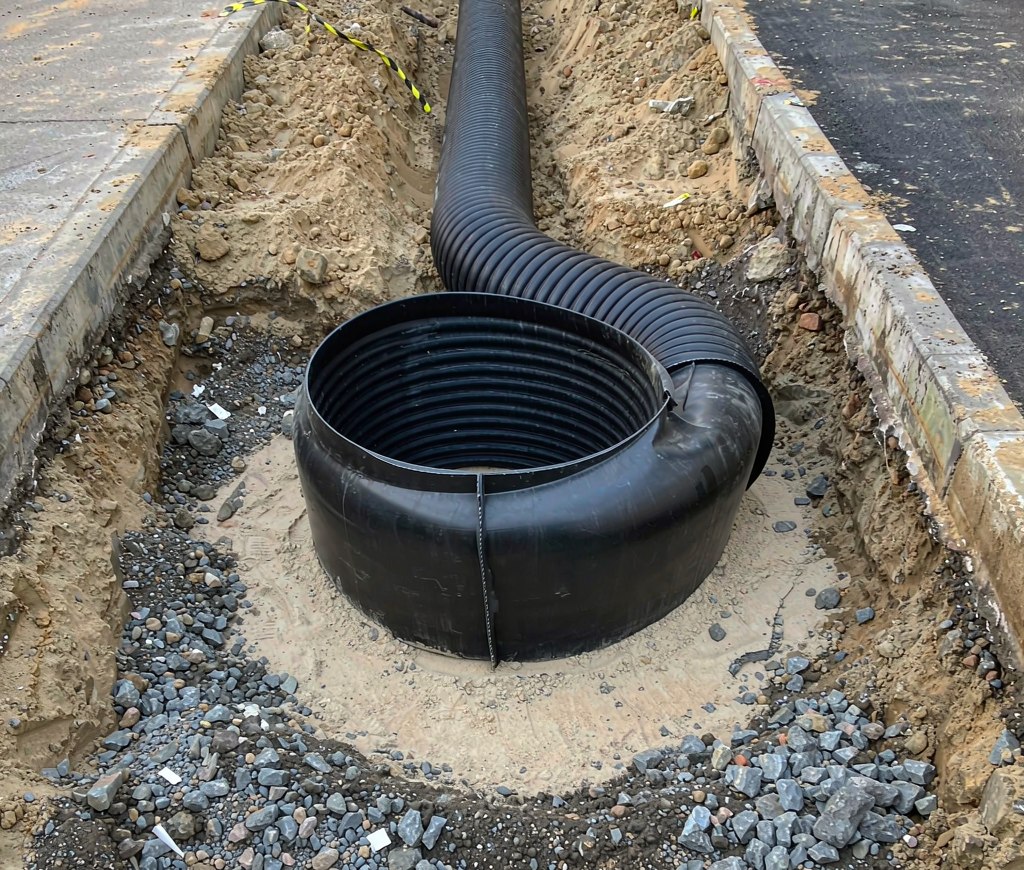
Flanges are used in valve wells, equipment interfaces, and parts that need to be disassembled: the flange surface and sealing groove should be cleaned, and the gasket should be made of oil resistant material according to the medium. It is strictly prohibited to use ordinary rubber gaskets to make up for the number; Tighten the bolts diagonally and evenly, with consistent force to compress the gasket evenly. If one side is tightened hard, the gasket will be squeezed out of one side, forming a leakage channel; The parallelism of the flange assembly should be calibrated, and bolts should not be forcefully pulled into place. There are still several leakage points in the sealing process: the direction and number of layers of the threaded transition piece wrapped with the raw material tape should follow the specifications, the sealing of the casing passing through the wall and the ground should be tight, and the gap between the casing and the pipeline should be filled according to the requirements of fire prevention and waterproofing. These sealing points are done carelessly, and leakage often starts from the wall root and the well wall.
After the installation of the pipeline network, conduct a comprehensive or segmented air tightness test: apply the specified pressure after sealing the end, observe the pressure drop changes, and ensure that the pressure remains stable during the stabilization period to be qualified; Isolate and inspect the pressure drop section by section, first check the joints and valves, and then check the pipe body. The testing pressure and holding time shall be carried out in accordance with the pipe process documents and design requirements. The testing records shall include pressure curve, ambient temperature, operator and reviewer, and shall be archived together with the completion data. The qualification of air tightness is a prerequisite for backfilling - both pressurized backfilling and backfilling before testing are methods of burying hidden dangers in the soil, and the acceptance sequence of concealed works cannot be reversed. On the daily maintenance end, the joints between the valve well and the operating well are inspected annually, and rusted and aged seals are replaced in advance.
| connection method | Applicable Part | Sealing points |
|---|---|---|
| Electric fusion socket | Buried main line | Scraping socket parameters in three steps |
| flange connection | Valve well equipment interface | Oil resistant pads are evenly fastened diagonally |
| Thread transition | Small caliber connectors | Specification for the number of layers in the direction of raw material belt |
| Casing sealing | Passing through walls and floors | Fill in to meet the requirements of fire and waterproofing |
| Breath holding test | Overall or segmented pipeline network | Stabilize the voltage and then backfill after passing the qualification |
| Document archiving | Welding parameters and curves | Completion data to be retained during testing |
Cannot: Parameters are bound to pipe fittings, pipe diameter, and ambient temperature, and are only set according to pipe fittings identification or process files as the correct path; The fusion interface, which is adjusted based on experience, has uncontrollable strength and sealing, and after completion, it becomes a hidden leakage point.
Most do not use: the electric fusion joint can be removed and re fused, and the flange joint can be replaced with a new gasket and tightened; After disposal, retest and close the air according to the same caliber, and merge the test records of the repair section into the original file. Do not leave any traces after repair.
Low temperature affects the welding quality and sealing elasticity: When the ambient temperature is lower than the requirements of the pipe process, insulation or adjustment measures should be taken according to the regulations. The sealing gasket should be of low temperature type, and the backfill soil should not contain frozen blocks to avoid settlement and stress in the joint area.
This article is organized by Luoyang wohong petrochemical equipment co., ltd. the company provides design, manufacture, installation, commissioning and operation and maintenance services for oil and gas recovery equipment, solvent recovery devices and buried composite pipe networks at gas stations, oil depots and chemical enterprises. if you need scheme configuration or on-site investigation, please contact and exchange.
 Previous articleHow many years can composite pipes last? What factors affect lifespan?
Next Why choose composite pipes for gas station pipeline renovation?
 Company Name:
Luoyang Wohong Petrochemical Equipment Co., Ltd
 Hotline:
13526990215
 Company Address:
W2-1, Dongda Technology Industrial Park, Luoxin Industrial Cluster, Xin'an County, Luoyang City
 E-mail
lixiang@vohonoilpipe.com
Scan to follow us
Luoyang Wohong Petrochemical Equipment Co., Ltd Powered by EyouCms Henan ICP Registration No. 17014668-11 sitemap.xml
 Product Category